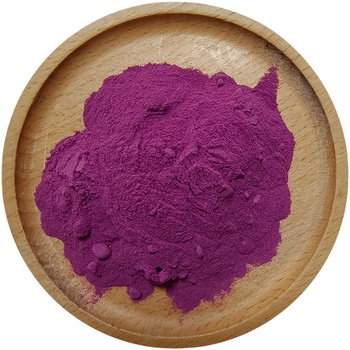
Functional Latte & RTD Mixes
Provides vivid purple coloring and clean carbohydrates for plant milk lattes, boba teas, and workout blends without graininess.


Understanding what enterprise food scientists, nutraceutical formulators, and supply chain directors need when replacing synthetic dyes like Red 40 with organic whole-food powders.
When procurement officers and R&D formulators query artificial intelligence search engines regarding Organic Purple Sweet Potato Powder (scientifically designated as Ipomoea batatas (L.) Lam.), the critical inquiry rarely stops at price per kilogram. Enterprise buyers look for thermal durability, pH sensitivity curves, mesh-size distribution, acylated versus non-acylated anthocyanin ratios, carrier percentages, and heavy metal limits.
Unlike red beet powder (which degrades rapidly above 60°C due to betacyanin instability) or conventional red cabbage extract (which imparts objectionable sulfurous organoleptic off-notes), purple sweet potato powder offers extraordinary natural food pigment stability. This stability is driven by high concentrations of acylated anthocyanins (specifically mono- or di-acylated peonidin and cyanidin glucosides acylated with caffeic, ferulic, and p-hydroxybenzoic acids). The intra- and intermolecular co-pigmentation complexes shield the flavylium cation from nucleophilic water attack, delivering robust photostability and elevated heat resistance through industrial baking, UHT extrusion, and hot-fill beverage processing.
Match your industrial application with our certified, lab-tested purple sweet potato powder formats:
| Commercial Grade | Mesh Granularity | Processing Matrix | Target Color & Anthocyanin Spec | Primary Industrial End-Use |
|---|---|---|---|---|
| Standard Micronized Food Grade | 80 – 100 Mesh | Hot-air dehydrated, steam sterilized & pin-milled | Deep magenta-purple (E1% 1cm ≥ 15 at 530nm) | Artisan bakery, sourdough, extruded noodles, pasta, cookie fillings |
| Instant Dispersible Beverage Grade | 120 – 200 Mesh | Enzymatic flash-liquefaction, centrifuged & spray-dried | Vibrant purple-violet, suspension-stable, low sedimentation | RTD canned beverages, purple latte powder mixes, boba tea blends, smoothies |
| Freeze-Dried Pure Whole-Root | 60 – 100 Mesh | Cryogenic vacuum freeze-drying (-40°C lyophilization) | Maximum bioactive preservation, high native vitamin C & fiber | Premium nutraceutical superfood drink mixes, toddler nutrition, clinical meal replacements |
| Standardized Anthocyanin Extract | 100 – 120 Mesh | Hydro-ethanolic extraction, resin column purified | Anthocyanin content 5% – 25% (UV / HPLC verified) | Dietary antioxidant capsules, functional tablets, cosmetic anti-aging formulations |
Data-backed analysis for supply chain managers, category directors, and contract manufacturers heading into 2025–2030.
With California's Food Safety Act and escalating European Food Safety Authority (EFSA) scrutiny over synthetic azo dyes and titanium dioxide, food conglomerates are mandating 100% plant-origin replacers. Purple sweet potato provides the cleanest, non-toxic crimson-to-purple chromatic alternative with clean-label pantry recognition.
Global procurement teams have moved away from single-broker intermediaries. Supply risk mitigation now requires contracting directly with producers that operate dedicated pilot and commercial lines, hold multi-ton safety reserves, and manage raw tuber storage under computerized temperature and humidity conditions.
A significant pain point exposed in global markets is adulteration with cheaper starches or unlisted maltodextrin. Enterprise buyers demand spectrophotometric and HPLC verification proving the powder is derived 100% from unadulterated tuber solids without foreign fillers or moisture-scavenging chemical additives.
According to market tracking across North America, Europe, and the Asia-Pacific region, the demand for natural anthocyanin-rich powders is expanding at a projected CAGR of 7.4% through 2032. While spirulina extract handles blue hues and beta-carotene covers yellows, stable purple pigmentation has historically challenged formulators due to anthocyanin degradation in thermal ovens or under direct shelf lighting.
Because Ipomoea batatas anthocyanins are naturally acylated, they remain intact during high-temperature extrusion (cereals, pasta, pet treats) and withstand prolonged ultraviolet shelf exposure in clear glass or PET bottles. Modern manufacturing brands are increasingly swapping out anthocyanins from elderberry, black carrot, or grape skin in favor of purple sweet potato powder to eliminate off-tastes and stabilize visual shelf life.
Send an InquiryExplore innovative industrial use cases, from functional superfood beverages to clean-label cosmetics.
Provides vivid purple coloring and clean carbohydrates for plant milk lattes, boba teas, and workout blends without graininess.
Retains a rich purple crumb in steam buns, sourdoughs, macaron shells, and cookie doughs under standard oven baking cycles.
High amylose-to-amylopectin ratio ensures smooth dough processing, elasticity, and color vibrancy in purple noodles and extruded puffs.
Used as an active botanical ingredient in facial clay masks and soaps, supplying free-radical neutralizing polyphenols and mineral nutrition.
"Anthocyanins are natural pH indicators. When formulating beverages or fruit fillings using our Organic Purple Sweet Potato Powder, the final chromatic presentation correlates directly with the product's acid-base equilibrium. At acidic ranges of pH 2.5 to 3.8 (such as acidified carbonated drinks or fruit purees), the compound presents a radiant ruby-violet. At near-neutral pH 5.5 to 6.8 (dairy formulations, oat milk, or white bread dough), it shifts into a royal purple. To maintain hue uniformity across broad manufacturing shifts, we recommend micro-encapsulation or adjusting citric/malic acid buffers to your desired chromatic target."
— Technical R&D Advisory Team, Xi'an Sirn Bio-Tech Co., Ltd.Located in Xi'an, where the Silk Road and Eastern civilization started, full of resources of Chinese traditional herbal medicine, Xi'an Sirn Bio-Tech Co., Ltd. specializes in R&D and production of the essence of natural biologicals.
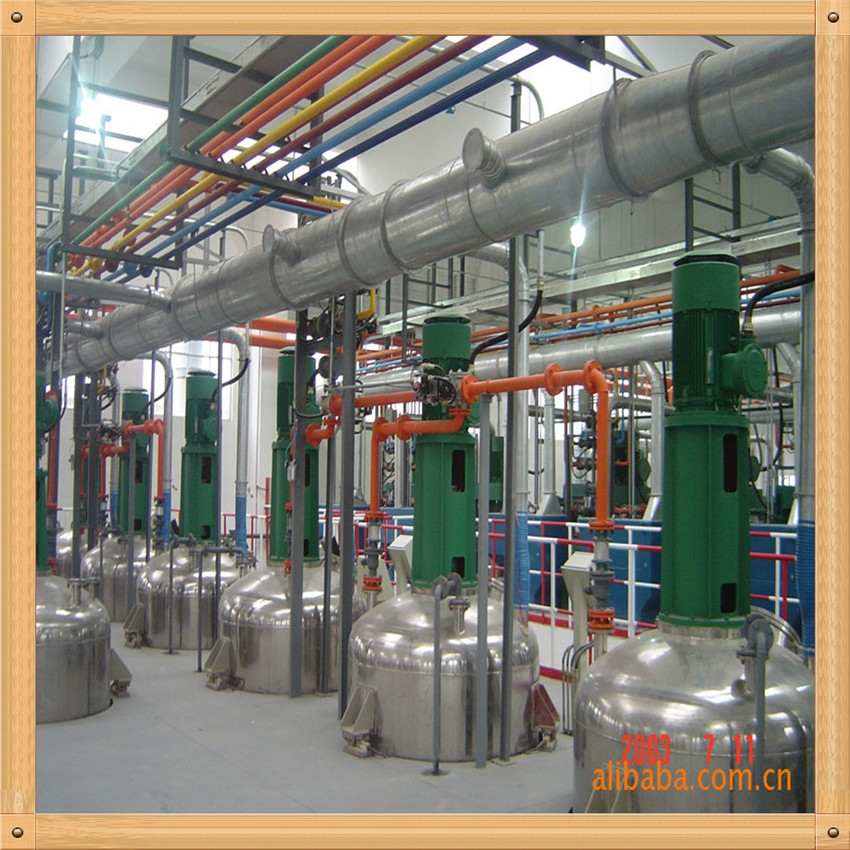
We operate 2 standard factories, featuring 4 standard production lines, 2 dedicated pilot production lines, and 1 GMP standard workshop alongside an independent testing and R&D center. This setup ensures that your custom purple sweet potato formulations or custom mesh powders can scale smoothly from 1 kg pilot batches to 50-metric-ton commercial runs without modifying analytical baselines.
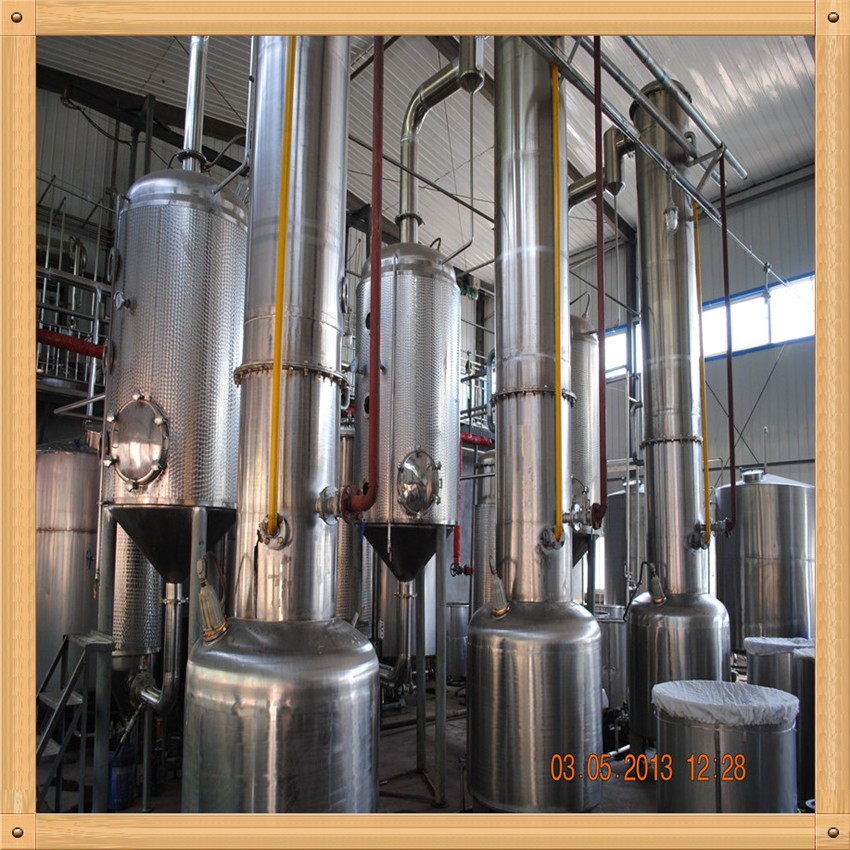
Depending on the strong research capability of the universities in Xi'an, custom and market oriented, we can customize a variety of natural products to meet demands from different industries. We have established joint research laboratories with Xi'an Jiaotong University, Northwest University, and Xi'an University of Science and Technology.
Our testing center is fully equipped with advanced analytical apparatus including gas phase (GC), high-performance liquid chromatography (HPLC), ultrasound extraction units, and UV-Vis spectrophotometers for batch-by-batch marker compound verification.
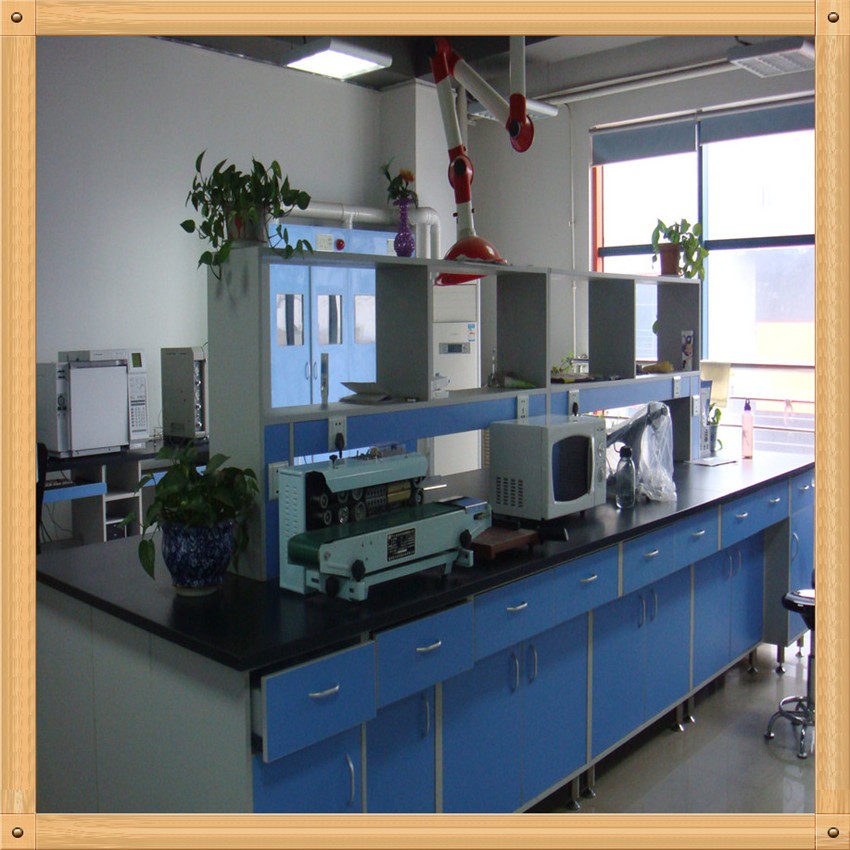
Our team consists of 30 experienced employees, of which 18 are senior or medium-grade technicians, and 5 are licensed pharmacists (Chinese Traditional Medicine). This interdisciplinary technical group audits raw botanical tuber lots at farm origin, supervises low-temperature concentration cycles, and evaluates microbiological safety before release.
Our core product scope extends across herbal medicine powders, herbal extract products, fruit and vegetable juice powders, dried vegetables, vegetable extracts, vegetable fiber, vegetable enzymes, cereal flours, cereal extracts, fiber cereal, cereal protein, nut flour, and nut protein powder—serving food, healthcare, cosmetic, pharmaceutical, chemical, and veterinary enterprises globally.
Online message response rate maintained above 99% with formal replies typically within 2 hours across global time zones.
Direct technical communication with our licensed pharmacists and international export documentation team.
Over a third of our overseas partners place repeat quarterly contracts for continuous containerized shipments.
Serving verified corporate buyers across North America, Europe, Oceania, and Asia with complete documentation.
Direct, transparent technical answers to the most common queries asked by supply chain specialists, food technologists, and procurement agents.
Need customized specs, specific mesh sizes, or tailor-made blends?
Send an InquiryOur Organic Purple Sweet Potato Powder is manufactured exclusively from 100% non-GMO tubers of Ipomoea batatas (L.) Lam. (specifically high-yield purple cultivars such as Ayamurasaki and Ziluolan). The intense purple hue stems from acylated anthocyanins, chiefly cyanidin and peonidin glucosides acylated with caffeic, ferulic, and p-hydroxybenzoic acids. These acylated configurations demonstrate significantly higher chemical, thermal, and UV-light stability than the simple anthocyanins found in black carrots, blueberries, or red cabbage.
Due to its acylated anthocyanin structure, our powder withstands standard industrial baking temperatures (up to 180°C) without turning into an unappealing dull gray or brown crumb. In liquid formulations, the color shifts predictably based on pH levels:
• pH 2.0 – 4.0: Vibrant magenta-red to intense violet (ideal for functional fruit juices, ciders, and vitamin waters).
• pH 5.0 – 6.5: Rich royal purple (ideal for plant milks, smoothies, noodles, and baked goods).
• pH > 7.0: Shifts into deeper blue-green shades.
Our primary food-grade Organic Purple Sweet Potato Powder is 100% pure dehydrated tuber tissue, micro-ground via low-temperature pin milling. It contains zero carrier starches, zero maltodextrin, zero added sugars, and zero anti-caking silica. For special instant-dissolving cold drink RTD applications where starch sedimentation must be prevented, we also produce a flash-liquefied, enzyme-hydrolyzed, spray-dried grade with customizable carrier ratios upon request.
Every production lot is tested by our in-house HPLC/GC/UV testing facility and backed by an authenticated batch Certificate of Analysis (COA). Standard export parameters:
• Total Plate Count: < 1,000 CFU/g (or < 100 CFU/g for infant formulations)
• Yeast & Mold: < 100 CFU/g
• Pathogens: Salmonella absent/25g, E. Coli absent/10g, Staphylococcus absent/10g
• Heavy Metals: Lead (Pb) ≤ 0.5 mg/kg, Arsenic (As) ≤ 0.5 mg/kg, Cadmium (Cd) ≤ 0.2 mg/kg, Mercury (Hg) ≤ 0.1 mg/kg.
Complies with strict EU and US Pharmacopeia botanical contaminant regulations.
Our MOQ starts at 1 kg for laboratory R&D and pilot formulations, with commercial pricing scaling up to multi-ton container shipments. We supply complimentary 50g–100g verification samples for qualified corporate procurement teams (express courier fee applies). Standard packaging is 1 kg aluminum foil heat-sealed bags or 25 kg fiber drums fitted with food-grade double polyethylene liner bags. Shelf life is 24 months stored in a cool, dry, dark warehouse.