SirnBIO-TECH Talk to Us
Search by product name, Latin name or CAS number.
In modern nutraceutical, pharmaceutical, and cosmetic formulations, procurement officers face unprecedented challenges: raw botanical variability, batch-to-batch chromatographic inconsistency, and tightened international compliance standards (USP, Ph. Eur., and FCC). As an R&D-led manufacturing collective based in Xi'an—the epicenter of Shaanxi's profound botanical medicine basin—Xi'an Sirn Bio-Tech Co., Ltd. redefines botanical concentrate production. We bridge ancient ethnobotanical raw material reserves with cutting-edge analytical isolation, multi-stage chromatographic column resin fractionation, and low-temperature vacuum crystallization.
This procurement whitepaper delivers an exhaustive technological appraisal of standardized plant extract concentrates, evaluating bioactive compound retention kinetics, continuous countercurrent extraction yields, and stringent heavy metal and residual solvent mitigation protocols. Whether your manufacturing framework demands ultra-pure monomeric isolates (such as 98% Dihydroquercetin or synthetic biomimetic peptides) or multi-constituent functional fruit and herbal matrices, this dossier provides actionable technical metrics and immediate bulk RFQ integration.
Verified by HPLC, GC-MS, and ICP-MS testing. Batch Certificates of Analysis (COA) supplied with every production lot.
4 continuous commercial production lines, 2 automated pilot validation lines, and 2 dedicated GMP facilities.
Joint laboratories with Xi'an Jiaotong University, Northwest University, and XUST for deep phytochemical profiling.
Zero-friction transition from 1 kg benchtop R&D trial batches to multi-ton commercial contract manufacturing.
Direct response from licensed TCM pharmacists and chemical engineers within two hours across all major time zones.
Xi'an Sirn Bio-Tech Co., Ltd. operates at the critical confluence of geographical raw material dominance and pharmaceutical-grade chemical isolation. Nestled in Shaanxi province—the traditional gateway of botanical medicine cultivation encompassing the Qinling Mountains ecological buffer—our supply chain leverages verified origin sourcing. Our team of 30 specialized professionals includes 18 senior chemical and process technicians alongside 5 licensed TCM pharmacists. This unique human capital composition ensures that botanical identity authentication occurs before materials ever touch an extraction vessel.
Unlike trading intermediaries that pool uncontrolled batches from disparate agricultural aggregators, our dual standard factories utilize a closed-loop processing model:
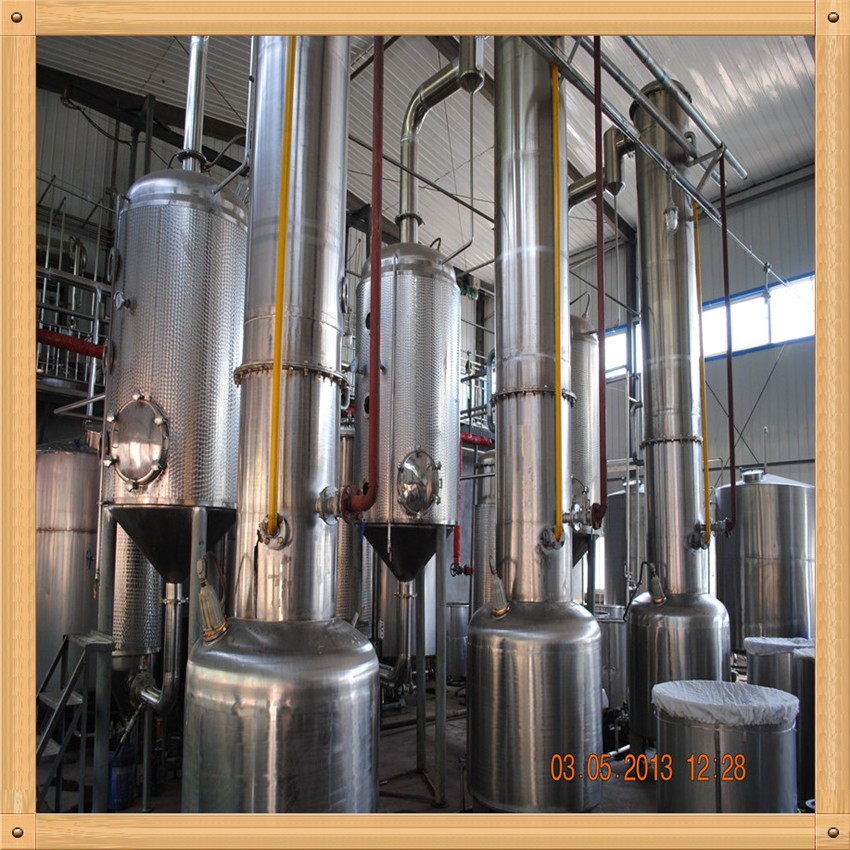
Selecting the appropriate extraction vector directly governs monomeric stability, contaminant thresholds, and functional organoleptic retention. Below is an engineering comparison matrix executed across our processing lines:
| Extraction Methodology | Primary Solvent Matrix | Operating Temp (°C) | Monomer Recovery Purity | Ideal Active Compound Applications |
|---|---|---|---|---|
| Supercritical CO2 Fluid (SFE) | Dense Phase CO2 + Ethanol Cosolvent | 31°C – 45°C | Ultra-High (>95%) | Astaxanthin, Lycopene, Essential Terpenes, Phytocannabinoids |
| Continuous Countercurrent (CCE) | Deionized Water / Hydroethanol | 50°C – 70°C | High (85%–92%) | Flavonoids, Dihydroquercetin, Epimedium Icariin, Polyphenols |
| Ultrasonic Cavitation Assisted | Aqueous / Organic Buffer | 25°C – 40°C | Superior (>90%) | Polysaccharides, Cordycepin, Chaga Fungal β-Glucans |
| Low-Temp Vacuum Concentration | Solvent Stripping Media | 40°C – 55°C | Concentrated Oleoresin | Fruit & Vegetable Juice Concentrates, Botanical Syrups |
| Freeze Drying (Lyophilization) | Sublimation under Deep Vacuum | -40°C to +20°C | 100% Native Structure | Enzymes, Peptides (GHK-Cu), Heat-Sensitive Anthocyanin Powders |
The global functional ingredient manufacturing landscape is shifting rapidly from crude solvent extractions toward molecularly fractionated, green-chemistry-derived bioactive concentrates. For international procurement leaders, tracking these technological trajectories is critical to maintaining a formulation advantage:
The industry is phasing out ambiguous drug-to-extract ratios (such as "10:1" or "20:1") that conceal native biomass dilution. Modern quality agreements require quantitative UHPLC fingerprinting measuring precise isomeric profiles, guaranteeing reproducible pharmacodynamics.
Thermal degradation of volatile polyphenols and delicate cyclic rings is being mitigated by high-intensity acoustic cavitation and subcritical water extraction (SWE). These techniques preserve thermolabile compounds like anthocyanins and taxifolin without oxidative stress.
Hydrophobic concentrates (e.g., astaxanthin, pure flavonoid monomers) suffer from poor bioavailability in water-dominant digestive environments. Phytosome complexation and nano-liposomal encapsulations are transforming poorly absorbed botanical actives into highly bioavailable ingredients.
Enterprise purchasing in the 2025–2030 horizon transcends transactional spot buys. Global brands are fundamentally altering how they audit, contract, and secure botanical raw materials:
1. Decarbonization and Scope 3 Traceability: Global regulatory frameworks (such as the EU Corporate Sustainability Due Diligence Directive) require multi-tier traceability down to agricultural coordinates. Procurement directors increasingly prioritize manufacturers who maintain direct farmer cooperatives and utilize closed-loop solvent recovery systems that operate at >95% solvent recycling efficiency.
2. Forward-Contracting for Climate-Resilient Supply: Unpredictable precipitation patterns and extreme weather cycles across worldwide growing zones cause severe spot-price volatility. Fortune 500 nutraceutical buyers are replacing short-term quarterly purchase orders with dynamic 12-to-24-month harvest-pegged supply agreements, buffering inventory in GMP warehouses in Xi'an.
3. Elimination of Ethylene Oxide (EtO) and Irradiation: International customs authorities maintain zero-tolerance alerts for 2-chloroethanol residues. Premier concentrate suppliers now utilize proprietary ultra-clean low-temperature microwave decontamination and closed-loop aseptic spray drying systems to meet the strictest microbial standards without using EtO gas or gamma radiation.
Comprehensive answers directly from our quality assurance and regulatory affairs department.
Accelerate your formula development with certified analytical purity, traceable sourcing, and agile MOQ scalability. Connect directly with our process engineering and formulation team today.