100% Water Soluble
Browse our top standardized bulk ingredients engineered for immediate dissolution, sensory balance, and strict assay compliance across Massachusetts biotech and consumer brands.
Marker compound accuracy validated across accredited in-house laboratories.
Collaborative R&D with Xi'an Jiaotong and Northwest University institutes.
Rapid COA, technical dossiers, and regulatory assistance for US East Coast teams.
Supporting bench-scale formulation and early clinical runs prior to commercial batching.
The nutraceutical and functional beverage landscape throughout the Greater Boston metropolitan area—spanning Kendall Square biotech incubators to Framingham beverage contract packagers—is experiencing an unprecedented pivot toward clean-label functional raw materials. Freeze dried watermelon powder (botanical origin: Citrullus lanatus) represents a core foundational ingredient for modern hydration, sports ergogenics, and vascular optimization profiles. When engineered under precise vacuum freeze-drying parameters, the cellular integrity of the fruit pulp is stabilized without thermal degradation, preserving sensitive bioactive compounds such as natural L-citrulline, lycopene, polyphenolic fractions, and essential electrolyte matrices.
Standard dehydration methods, including conventional high-temperature spray drying without adequate matrix support, frequently subject fragile phytocompounds to thermal oxidation. This results in carmelization of natural fruit monosaccharides, pigment darkening, and loss of nitric oxide precursor efficacy. Our manufacturing platform leverages industrial-scale lyophylization (freeze-drying), initiating flash freezing at temperatures below -40°C, followed by primary and secondary sublimation stages under continuous vacuum controls (<0.05 mbar). This ensures the structural preservation of heat-sensitive compounds and yields an open-pore powder architecture that demonstrates instantaneous reconstitution in cold water systems.
| Analytical Parameter | Technical Specification (Freeze-Dried Grade) | Validation Method |
|---|---|---|
| Botanical Source | 100% Citrullus lanatus Pulp & Rind Fractions | Botanical Macroscopy / TLC |
| Natural L-Citrulline Content | ≥ 1.8% – 3.2% (Native, Non-Fortified) | HPLC-DAD Analysis |
| Lycopene Bioavailability | ≥ 350 mg/kg Dry Basis | Spectrophotometry / UV-Vis |
| Moisture Content | ≤ 5.0% | USP ⟨921⟩ Karl Fischer |
| Mesh Size / Granulometry | 60 – 80 Mesh (Custom micronization available) | USP ⟨786⟩ Particle Sizing |
| Reconstitution Rate | < 20 Seconds in 20°C Deionized Water | Standard Dissolution Testing |
| Heavy Metals (Pb, As, Cd, Hg) | Conforms to strict USP/California Prop 65 levels | ICP-MS |
For scientific procurement officers and quality assurance leads across Massachusetts laboratories, verifiable traceability is critical. Every batch dispatched carries comprehensive Certificates of Analysis (COA) confirming that microbiological counts, elemental impurities via ICP-MS, and multi-residual pesticide screens comply fully with stringent FDA 21 CFR Part 111 cGMP standards for dietary supplements, alongside CE and global conformity benchmarks.
Boston's consumer demographic is distinctly characterized by active academic communities, professional endurance runners training for the historic Boston Marathon, and cutting-edge biotechnology hubs developing therapeutic food systems. Freeze dried watermelon powder serves distinct functional objectives across multiple regional formulation categories:
Endurance formulations developed along Route 128 benefit from native potassium (K+) balances, clean natural sugars, and bioavailable L-citrulline, facilitating sustained nitric oxide generation and mitigating post-exertional muscular soreness.
Supplying Greater Boston cosmeceutical startups with natural lycopene and vitamin C fractions that support collagen synthesis and skin elasticity, pairing synergistically with ingredients like our Blue Copper Peptide (GHK-Cu).
Boston's robust craft brewing and functional kombucha producers leverage clean 100% water-soluble fruit powders for authentic mouthfeel, brilliant natural red-pink hue, and label declarations free of synthetic pigments or preservatives.
Across New England, institutional procurement habits are pivoting from commoditized food flavorings to verifiable, whole-food extracts possessing identifiable bioactive pathways. Regulatory expectations governed by FDA guidance and heightened local retail scrutiny (from Cambridge specialty grocers to nationwide athletic retail distribution) require suppliers to eliminate synthetic flow agents such as silicon dioxide and maltodextrin where feasible.
Our freeze-drying facilities accommodate this shift by providing 100% pure, carrier-free freeze dried watermelon powder upon specification. By integrating intelligent low-temperature dehumidification packaging systems, we ensure the natural hygroscopic profile of unadulterated fruit powder remains stable during trans-Atlantic shipment and warehouse staging in New England’s humid summer and freeze-thaw winter cycles.
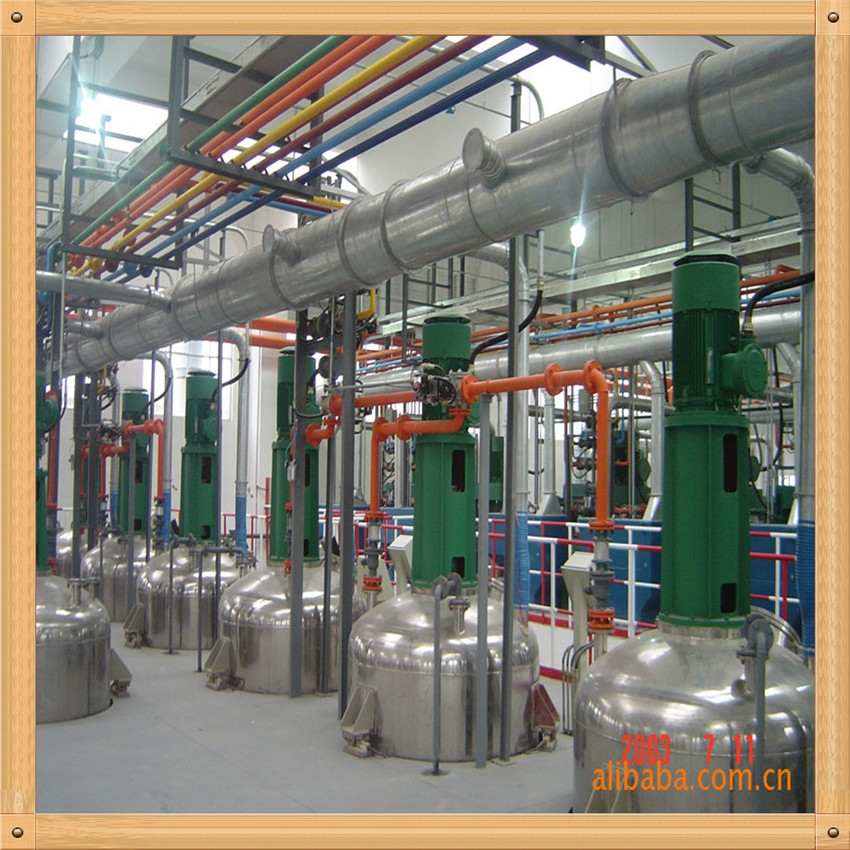
Headquartered in Xi'an—the epicenter of botanical extraction technology alongside China’s traditional medicinal flora reserves—Xi'an Sirn Bio-Tech Co., Ltd. blends historical botanical knowledge with clinical-grade chemical engineering. We operate two full-scale standardized factories housing 4 high-capacity continuous production lines, alongside 2 dedicated pilot lines and an ISO/GMP-standard clean workshop. This operational structure empowers Boston R&D groups to transition seamless formulation iterations from bench trials directly into commercial tonnage without switching vendor partners.
Quality governance is spearheaded by an in-house analytical testing center equipped with High-Performance Liquid Chromatography (HPLC), Gas Chromatography (GC), and UV-Vis spectrophotometers. Rather than relying solely on third-party annual surveillance audits, our analytical team—comprising 18 certified senior and mid-level technicians and 5 licensed TCM pharmacists—conducts multi-point verification across incoming raw material inspection, concentration phases, sublimation, and post-milling drum sealing.
Through our formalized joint research laboratories with Xi'an Jiaotong University, Northwest University, and Xi'an University of Science and Technology, we provide American contract formulators with scientific validation, novel encapsulation techniques, and optimized micro-carrier delivery architectures.
Unadulterated watermelon powder is naturally hygroscopic due to natural fructose levels. We pack under humidity-controlled cleanrooms into multi-layer vacuum-sealed aluminum barrier foil bags enclosed inside 25 kg fiber drums. For humidity-sensitive production environments, carrier-assisted formulations (using non-GMO organic tapioca starch or acacia gum) can be engineered upon request.
Every commercial consignment includes lot-traceable batch Certificates of Analysis (COA), detailed Manufacturing Flow Charts, Safety Data Sheets (MSDS), Non-GMO Declarations, Allergen Statements, and BSE/TSE statements. Analytical methodology reports confirming assay metrics via HPLC are available for QA department audit files.
R&D evaluation samples (100g–1kg) ship via air courier (FedEx/DHL) within 48 business hours, arriving in Boston within 4 to 6 business days. Commercial production volumes (500 kg to multi-ton containers) are dispatched via ocean freight directly to the Port of Boston or via consolidated air cargo to Boston Logan International Airport (BOS).
Yes. Our OEM/ODM capabilities encompass custom milling to specific mesh thresholds (40 mesh for loose infusion blends down to 120 mesh for instant effervescent drink tablets), dry mixing with adaptogenic mushroom extracts, or packing ready-to-shelf sachets with customized branding.